
Hi, I'm Dave. After spending 25 rewarding years in sales, I took a step back for health reasons and embarked on a new journey of creativity and innovation. In 2017/18, I bought a 3D printer and delved into the world of CAD, designing my own unique creations. This passion for design and craftsmanship led me to build a Workbee CNC from a kit and explore the realm of CAM.
A few years down the line, I upgraded to a custom CNC and expanded my arsenal of machines. Today, I proudly operate a compact yet efficient garage workshop where I bring my designs to life. Under the name "GoodWood," I enjoy making and selling my handcrafted creations. This new venture has kept me engaged, inspired, and excited about the endless possibilities of what I can create next.
You can follow my maker antics here: https://linktr.ee/GoodWoodEmporium
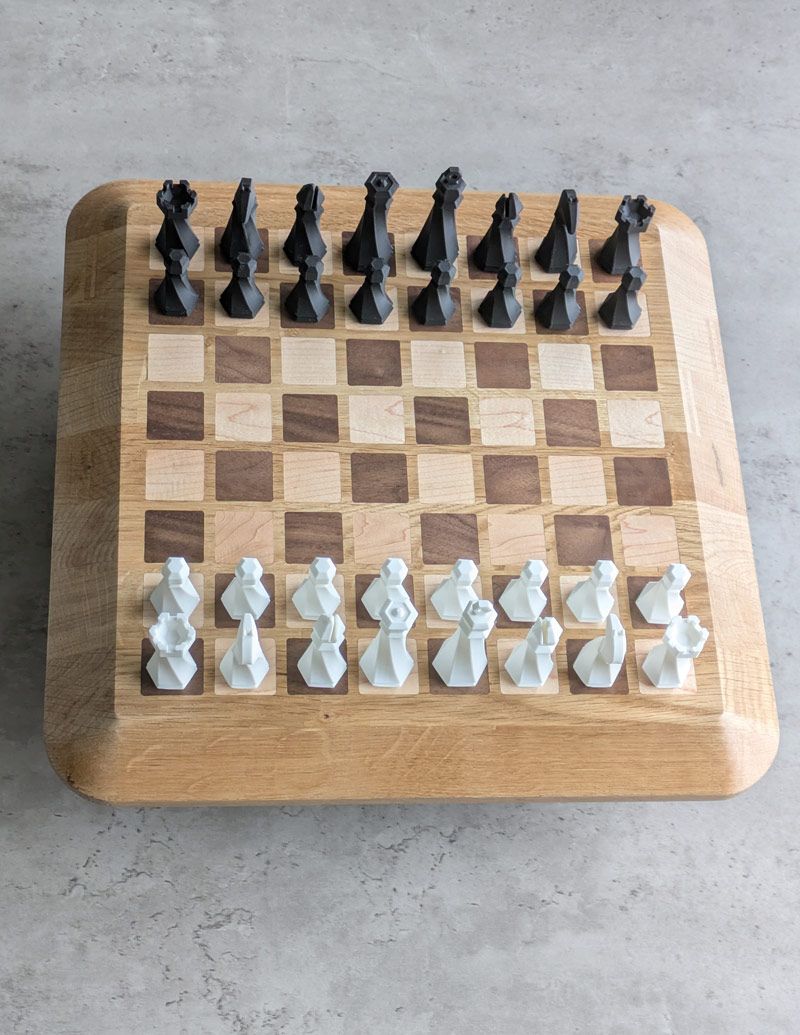
Présentation du projet
Cet échiquier a été réalisé à partir d'une chute de plan de travail en chêne de taille moyenne, avec des incrustations en noyer et en érable pour les cases alternées. La précision de la technique d'incrustation VCarve, calculée dans Vectric Aspire, a permis d'obtenir une finition impeccable et professionnelle.
Conception et flux de travail
Les trajectoires d'outil VCarve pour l'incrustation ont été initialement générées dans Aspire, puis la disposition des cases a été ajustée à l'épaisseur du bois disponible. Un recalcul a été effectué pour optimiser le placement et garantir un ajustement précis.
En raison des variations d'épaisseur entre les deux essences de bois, le collage des incrustations a été réalisé en deux étapes. Une fois assemblé, toutes les surfaces ont été poncées, scellées et finies avec un vernis polyuréthane appliqué au chiffon pour une surface lisse et durable.
Points clés à considérer
Un décalage de limite a été appliqué aux trajectoires d'ébauche et de finition 3D afin de contrôler la profondeur de découpe du profil de la carte. Cela a laissé une profondeur d'environ 3 mm pour la découpe finale du profil avec languettes.If modifying the finishing tool size, the boundary offset must be adjusted accordingly (e.g., an 8mm ball nose requires a 3mm offset, whereas a 6mm ball nose would need a 2.8mm offset).
Cutting Tools Used
3.175mm Endmill - VCarve inlay socket & plug clearance
60° V-Bit - VCarve inlay socket & plug cutting
6mm Endmill - 3D clearance & profile cutting
8mm Ball Nose - 3D finishing
32mm Surfacing Bit - Flattening stock & inlaid squares
Additional Tools
Bandsaw - Separating inlaid squares
Clamps - Securing glue-up
Aspire Features Utilized
3D Modeling – Created the angular shape for the board.
V-Inlay Toolpath – Ensured precise inlay fitting.
Tool Keep-Out Zones – Defined areas to control tool movement and cutting boundaries.
Material Requirements
Oak Worktop - 400 x 400 x 30mm - Flattened on CNC before starting
Hardwood Boards (Light & Dark) - 650 x 84 x 15mm (x2) -Pre-flattened before machiningCe projet met en valeur la puissance de la fonction d'incrustation VCarve d'Aspire et souligne la précision de l'usinage CNC dans le travail du bois de haute qualité. Il en résulte un jeu d'échecs artisanal d'exception, alliant l'élégance des matériaux à une maîtrise parfaite de l'usinage.

Convient à la version 12 ou plus
Login to V&Co to download the files
Se connecterPlease access this page on a desktop computer to download the files

Vectric Ltd
Precision House
2 Arden Road
Alcester
B49 6HN
Immatriculée en Angleterre sous le numéro 05382596
Immatriculation à la TVA GB115123072
Politique de confidentialité |
Politique relative aux cookies |
Termes et conditions



